For EPC contractors and end users, high-performance alloy pipes are not ordinary commodities. Materials such as titanium, Alloy 625, Alloy 825, Hastelloy C-276, Monel 400, duplex stainless steel, and super duplex stainless steel are often used in desalination, LNG, chemical processing, power plants, refineries, offshore platforms, and heat exchanger systems.
In these applications, one wrong material, one missing test report, one dimensional deviation, or one damaged package can delay the whole project.
That is why “zero-defect delivery” should not be treated as a slogan. It must be built through a controlled process: material verification, production control, inspection planning, NDT, MTC review, third-party inspection, packing protection, and final document checking before shipment.
This guide explains how buyers and suppliers can reduce rejection risk and achieve reliable delivery for high-performance alloy pipe and tube projects.
Quick Answer
Zero-defect delivery for alloy pipes means that the delivered material matches the purchase order, project specification, applicable standard, inspection requirement, and final documentation requirement.
It does not happen only at final inspection. It starts before production.
A reliable delivery process should control:
- Correct material grade and UNS number
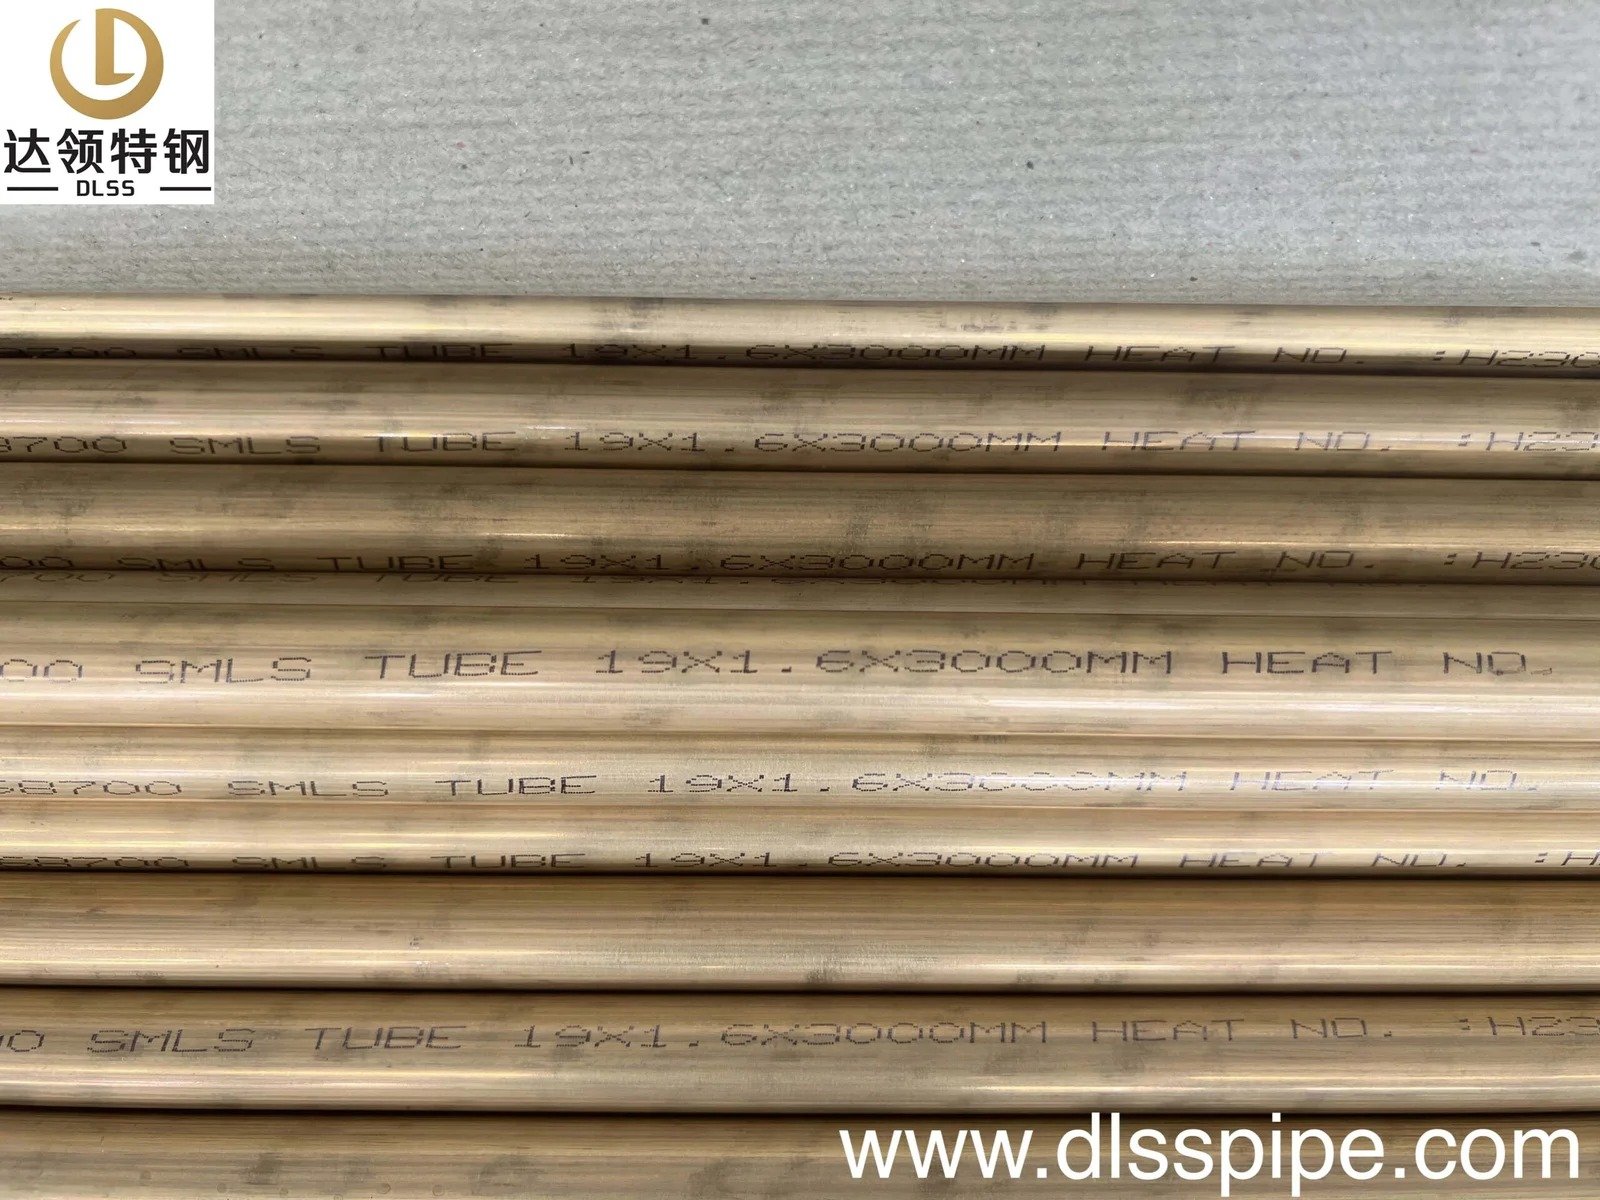
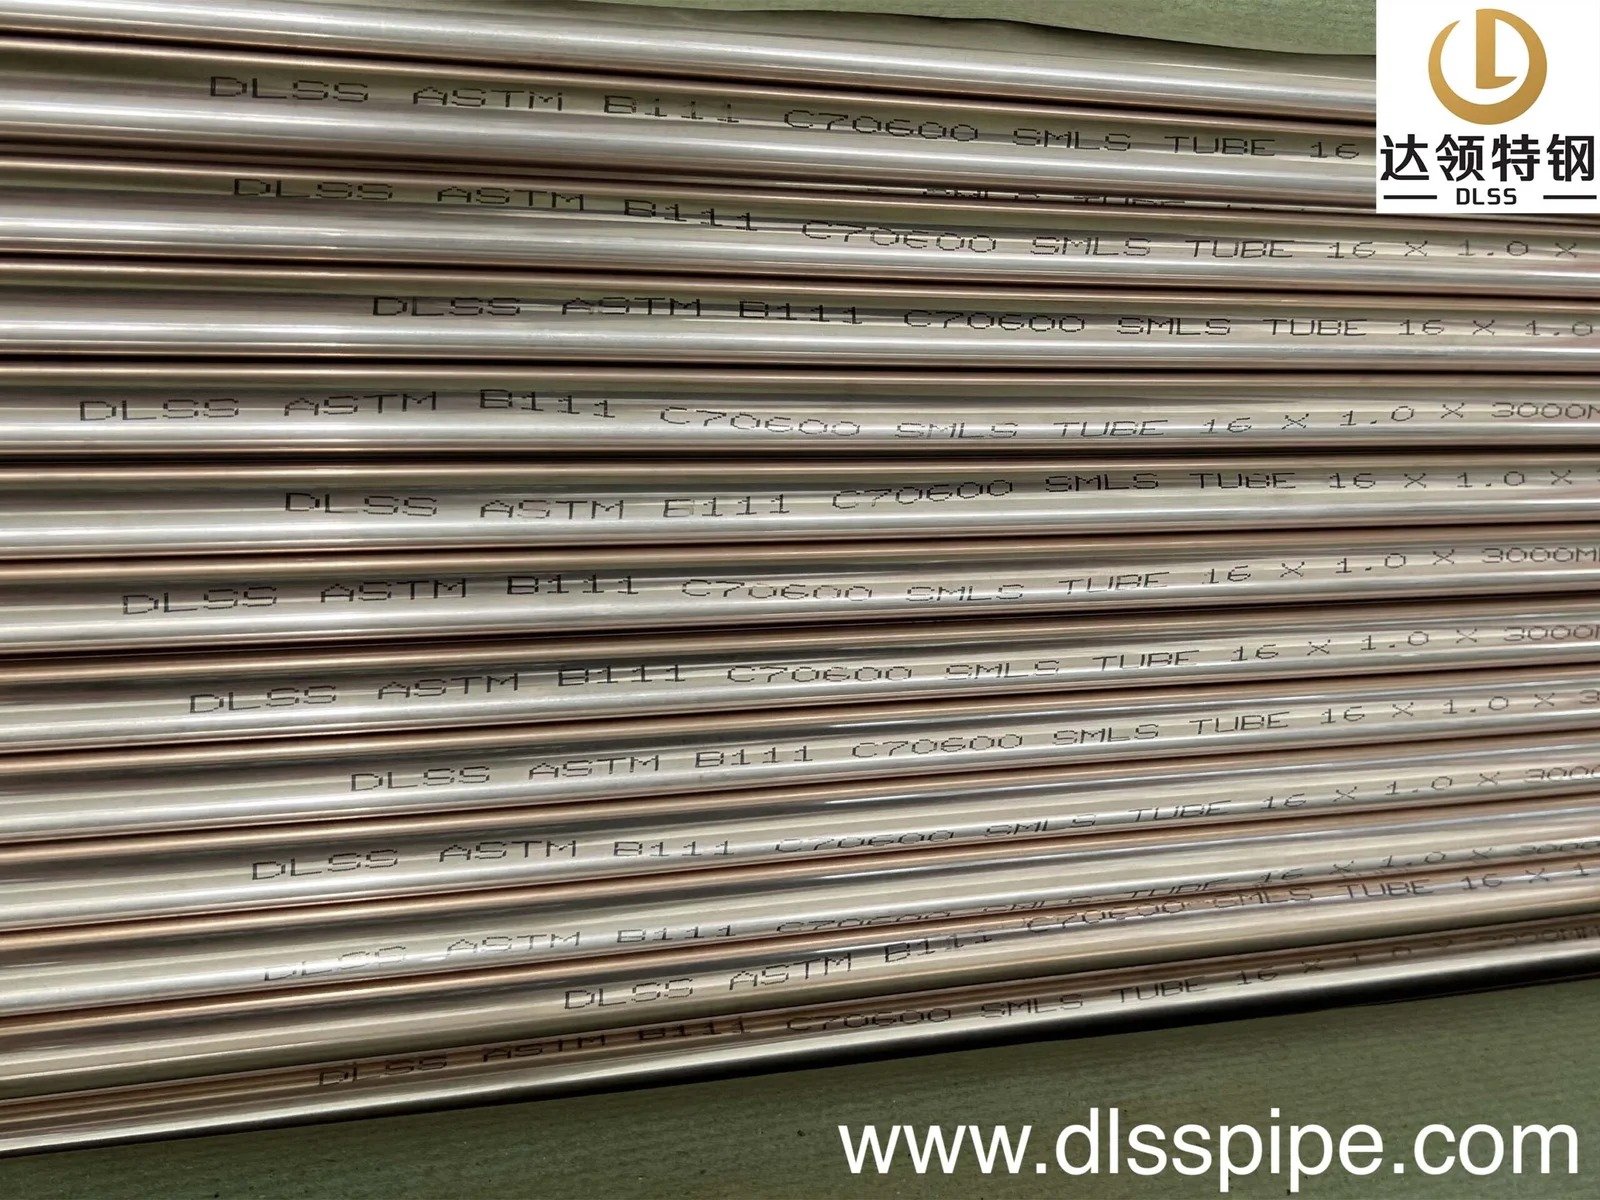
- Heat number traceability
- Chemical composition and mechanical properties
- Dimensional tolerance
- Heat treatment condition
- Surface condition
- NDT and hydrostatic test
- PMI verification
- MTC and inspection documents
- Third-party inspection witness, if required
- Export packing and shipment protection
For critical alloy pipe projects, quality should be planned in the RFQ and PO stage, not corrected after production.
Why Alloy Pipe Delivery Has Higher Risk
High-performance alloy pipes are often used in critical systems where failure is expensive. Compared with common carbon steel or standard stainless steel, alloy pipes usually have higher material cost, longer lead time, stricter inspection requirements, and more complex documentation.
Common risks include:
- Wrong alloy grade
- Mixed heat numbers
- Missing traceability
- Incorrect wall thickness
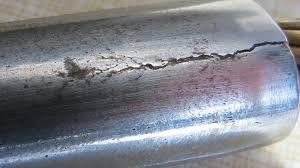
- Surface defects
- Incomplete heat treatment record
- NDT not performed as required
- MTC does not match PO
- Missing EN 10204 3.1 or 3.2 certificate
- Third-party inspection not arranged in time
- Material damage during packing or transportation
For EPC projects, these problems do not only affect the supplier. They may also delay installation, commissioning, and final handover.
Step 1: Confirm Material Grade and Standard Before Production
The first step is to confirm the exact material requirement. “Nickel alloy pipe” or “titanium tube” is not enough for production.
The RFQ and PO should clearly state:
- Material grade
- UNS number
- Standard
- Size
- Wall thickness
- Length
- Product form: pipe, tube, U-tube, fitting, or flange
- Seamless or welded type
- Heat treatment condition
- Testing requirement
- MTC requirement
- Third-party inspection requirement
For example, Alloy 625 should be confirmed as UNS N06625. Alloy 825 should be confirmed as UNS N08825. Hastelloy C-276 should be confirmed as UNS N10276. Titanium Grade 2 should be confirmed according to the applicable standard and project specification.
A good supplier should not start production based on incomplete material descriptions. If the specification is unclear, it should be clarified before raw material preparation.
Step 2: Keep Full Heat Number Traceability
Traceability is one of the most important parts of alloy pipe quality control.
Each pipe or tube should be traceable to the correct heat number. The heat number connects the physical material with the chemical composition, mechanical properties, heat treatment record, and MTC.
During production and inspection, the supplier should control:
- Heat number marking
- Batch separation
- Material transfer records
- Cutting records
- Testing records
- Final packing list
- MTC matching
For mixed-size or multi-grade orders, traceability control is even more important. A small mixing mistake can cause serious project rejection.
Before shipment, buyers should check whether the heat number on the material, packing list, MTC, and inspection report is consistent.
Step 3: Control Production Process, Not Only Final Inspection
Final inspection can find problems, but it cannot always fix them without delay. For critical alloy pipe projects, process control is more important than end-point checking.
The supplier should control:
- Raw material condition
- Forming or cold working process
- Heat treatment process
- Straightness
- End preparation
- Surface finish
- Pickling or passivation, if required
- Dimensional tolerance
- Marking
- Cleaning
- Packing preparation
For nickel alloy, titanium, duplex, and super duplex materials, heat treatment and surface condition should be handled carefully. Poor process control may lead to dimensional problems, surface defects, corrosion risk, or documentation disputes.
Buyers should ask the supplier to confirm key process steps before production when the project is critical.
Step 4: Build a Clear Inspection and Test Plan
An Inspection and Test Plan, or ITP, helps align the buyer, supplier, end user, and third-party inspector before production.
A good ITP should define:
- Inspection stage
- Test item
- Acceptance standard
- Witness point
- Hold point
- Responsible party
- Required document
- Final review requirement
For high-performance alloy pipes, common inspection items may include:
- Visual inspection
- Dimensional inspection
- Wall thickness measurement
- Chemical composition check
- Mechanical test
- PMI
- Hydrostatic test
- Eddy current test
- Ultrasonic test
- Surface inspection
- Heat treatment record review
- MTC review
- Third-party inspection witness
- Final packing inspection
The ITP should be confirmed before production. If the buyer requests third-party inspection only after the goods are ready, it may cause delay or repeated testing.
Step 5: Use NDT Based on Project Risk
NDT is a key part of alloy pipe delivery. The correct NDT method depends on the product type, material, size, wall thickness, and project specification.
Common NDT methods include:
- Ultrasonic testing
- Eddy current testing
- Hydrostatic testing
- PMI
- Dye penetrant testing
- Visual inspection
- Dimensional inspection
Ultrasonic testing is commonly used to detect internal or volumetric discontinuities in metal pipe and tubing. Eddy current testing is often used for tubes, especially heat exchanger tubes, depending on the applicable standard and project requirement.
For critical applications, the NDT requirement should be written clearly in the PO. The supplier should confirm the test method, acceptance level, inspection percentage, and reporting format before production.
A simple sentence like “standard test required” is not enough for high-risk alloy projects.
Step 6: Review MTC Before Shipment
For alloy pipe projects, the MTC is not just a document. It is the proof that the delivered material matches the order requirement.
Before shipment, buyers should check:
- Supplier name
- Buyer name or PO number
- Material grade
- UNS number
- Standard
- Heat number
- Size and quantity
- Chemical composition
- Mechanical properties
- Heat treatment condition
- NDT results
- Hydrostatic test result, if required
- PMI result, if required
- Third-party inspection stamp, if required
- EN 10204 3.1 or 3.2 certificate type, if required
For 3.2 inspection projects, third-party inspection should be arranged before or during the agreed inspection stage. It should not be treated as a document that can simply be added after shipment.
If the MTC does not match the PO, the buyer should ask for correction before goods leave the factory.
Step 7: Protect the Material During Packing and Shipment
Even if the material passes all tests, poor packing can still create delivery problems.
Alloy pipes and tubes may be damaged by:
- Surface scratches
- End deformation
- Moisture
- Salt exposure
- Poor wooden case strength
- Loose bundling
- Mixed heat numbers
- No end protection
- Rough loading and unloading
For export delivery, packing should consider:
- Material value
- Tube length
- Wall thickness
- Surface finish
- Shipping route
- Container loading
- Lifting points
- Moisture protection
- End caps or end protection
- Clear shipping marks
- Packing list consistency
For bright annealed tubes, precision tubes, titanium tubes, nickel alloy tubes, and heat exchanger tubes, packing protection should be confirmed before shipment.
What Buyers Should Include in the RFQ
A clear RFQ helps reduce quality disputes.
Buyers should provide:
- Material grade and UNS number
- Applicable standard
- Pipe or tube size
- Quantity
- Seamless or welded requirement
- Application and service condition
- Design pressure and temperature
- Corrosion medium
- Heat treatment requirement
- Surface finish requirement
- NDT requirement
- Hydrostatic test requirement
- PMI requirement
- MTC type
- EN 10204 3.1 or 3.2 requirement
- Third-party inspection requirement
- Packing requirement
- Delivery schedule
- Project specification or drawing
If the buyer is not sure which inspection items are necessary, the RFQ can state:
“Please review the attached project specification and recommend a suitable inspection and test plan for alloy pipes, including material traceability, NDT, PMI, MTC, third-party inspection, and packing requirements before quotation.”
How DLSS Controls Alloy Pipe Delivery Risk
At DLSS, alloy pipe delivery is controlled from order review to final shipment. Our goal is to help buyers reduce technical risk, documentation risk, and delivery risk.
Our control process includes:
- Specification review before quotation
- Material grade and UNS number confirmation
- Standard and size confirmation
- Raw material traceability check
- Production process control
- Heat treatment and surface condition review
- Dimensional inspection
- PMI, NDT, or hydrostatic test coordination
- MTC and document review
- Third-party inspection support when required
- Packing inspection before shipment
- Final document package preparation
DLSS can support stainless steel, duplex, super duplex, nickel alloy, titanium, copper alloy, and other high-performance alloy pipes and tubes for heat exchangers, chemical plants, desalination, LNG, oil and gas, shipbuilding, power plants, and industrial projects.
Common Mistakes Buyers Should Avoid
Mistake 1: Confirming Inspection Too Late
Inspection requirements should be confirmed before production. Late requests may cause delay, extra cost, or incomplete documentation.
Mistake 2: Only Checking Price
For alloy pipes, the cheapest quotation may not include the same testing, documentation, packing, or third-party inspection scope.
Mistake 3: Using Vague Material Descriptions
Terms like “nickel alloy pipe” or “titanium tube” are too general. The RFQ should include grade, UNS number, standard, size, and condition.
Mistake 4: Ignoring Heat Number Traceability
If heat numbers are mixed or not clearly marked, the material may fail final document review even if the physical product looks correct.
Mistake 5: Treating Packing as a Minor Detail
For long-distance export, packing is part of quality control. Damaged ends, scratched surfaces, or mixed bundles can create problems at the job site.
FAQ
What does zero-defect delivery mean for alloy pipes?
It means the delivered material matches the PO, project specification, standard, inspection requirement, and document requirement, with no critical quality or documentation issue at final acceptance.
Can any supplier truly guarantee zero defects?
A supplier should not rely only on promises. Defect risk is reduced through material traceability, process control, inspection planning, NDT, MTC review, third-party inspection, and proper packing.
Why is MTC review important?
The MTC proves material identity, heat number, chemical composition, mechanical properties, test results, and conformity to the order. For critical alloy projects, incomplete MTCs can delay final acceptance.
When is third-party inspection needed?
Third-party inspection is usually needed when the project specification, end user, EPC contractor, or regulation requires independent witness or certification. It should be confirmed before production.
What should I send to DLSS for a quality-controlled quotation?
Please send the material grade, UNS number, standard, size, quantity, application, service medium, pressure, temperature, inspection requirement, MTC requirement, third-party inspection requirement, packing requirement, and delivery schedule.
Conclusion
Zero-defect delivery for high-performance alloy pipes is not achieved by final inspection alone. It requires a controlled process from specification review to raw material traceability, production control, NDT, MTC review, third-party inspection, packing, and final shipment.
For EPC contractors and end users, the safest approach is to define quality requirements early. The RFQ and PO should clearly state material grade, standard, inspection scope, MTC type, third-party inspection, and packing requirements.
DLSS supports high-performance alloy pipe and tube projects with material review, production coordination, inspection support, MTC documentation, third-party inspection, and export packing. If your project requires titanium tubes, nickel alloy pipes, duplex stainless steel, super duplex stainless steel, or other special alloy materials, our team can help review your specification before production and prepare a reliable delivery plan.