Top 5 Desalination and Chemical Projects Using Titanium and Nickel Alloy Tubes

DLSS - Pipe&Tube - Top 5 Desalination and Chemical Projects Using Titanium and Nickel Alloy Tubes

1. Introduction

Titanium tubes and nickel alloy pipes are increasingly used in large-scale desalination and chemical processing projects worldwide. Their resistance to chloride-rich seawater and aggressive acids makes them indispensable in critical applications. Below are five landmark projects where titanium and nickel alloy piping solutions have proven their value.


2. Shuaibah 3 IWP – Saudi Arabia (Desalination)

  • Material Used: Titanium GR2 condenser tubes (ASTM B338).
  • Reason: Resistance to seawater corrosion and biofouling.
  • Scale: One of the largest desalination plants in the Middle East, producing over 600,000 m³/day.
  • Outcome: Titanium ensured long-term reliability and reduced maintenance costs.

3. Jubail 3A Desalination Plant – Saudi Arabia (Desalination)

  • Material Used: Titanium GR12 tubes, U-bend configuration.
  • Reason: Withstand high chloride brine and elevated temperature.
  • Scale: Over 570,000 m³/day water output.
  • Outcome: Titanium tubes achieved projected lifespan of 25+ years with minimal failures.

4. Reliance Industries – India (Chemical Processing)

  • Material Used: Inconel 625 and Hastelloy C-276 pipes.
  • Reason: Handle sulfuric and hydrochloric acid streams in hydroprocessing units.
  • Scale: One of the world’s largest refinery complexes.
  • Outcome: Nickel alloys eliminated frequent leakage issues of stainless steel alternatives.

5. BASF Chemical Complex – Germany (Chemical Industry)

  • Material Used: Incoloy 825 tubes (ASTM B423).
  • Reason: High resistance to phosphoric and sulfuric acids.
  • Scale: Multi-unit chemical plant modernization project.
  • Outcome: Longer service life and reduced downtime, ensuring process safety.

6. Fujairah Desalination Plant – UAE (Desalination)

  • Material Used: Titanium condenser tubes in MED (Multi-Effect Distillation) system.
  • Reason: Excellent seawater corrosion resistance and lifecycle savings.
  • Scale: Supplies millions of gallons of potable water per day to UAE.
  • Outcome: Titanium adoption lowered lifecycle cost compared to copper alloys.

7. DLSS Contribution to Similar Projects

At DLSS, we have supplied titanium and nickel alloy pipes for desalination and chemical projects with:

  • ASTM B338 titanium tubes (GR2/GR12).
  • ASTM B444 Inconel 625, ASTM B423 Incoloy 825, ASTM B622 Hastelloy C-276 pipes.
  • Third-party inspection (TÜV, DNV, LR).
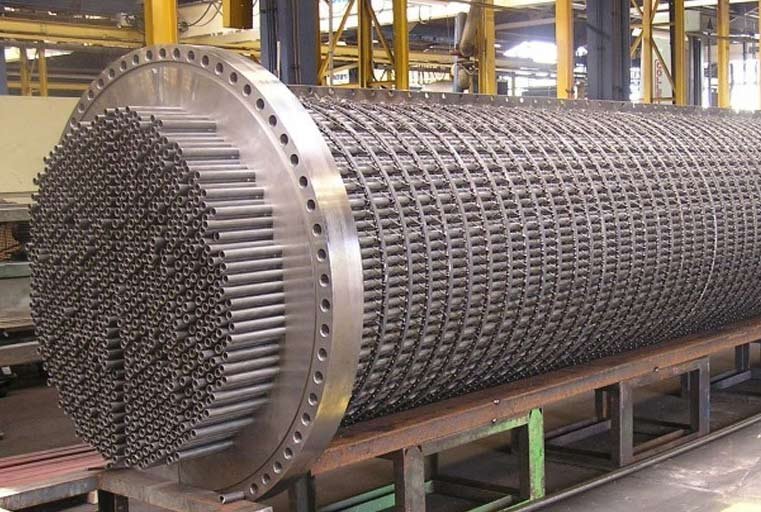
  • Custom fabrication including U-bend tubes and large-diameter pipes.

8. Conclusion & Call to Action

From Middle Eastern desalination plants to European chemical complexes, titanium and nickel alloy tubes have proven indispensable in extending service life and ensuring safe operations. As global demand grows, EPC contractors and end-users are increasingly turning to these high-performance alloys.

DLSS stands ready to support your projects with zero-defect, ASTM-compliant alloy pipes and tubes.

Contact us today for project support and quotations.
info@dlsspipe.com | www.dlsspipeline.com
Wonderful! Share This Case:

Austenitic Stainless Steel

Duplex Stainless Steel

Nickel Alloys

▪ Incoloy Family

▪ Inconel Family

▪ Monel Family

▪ Hastelloy Family

▪ Other Special Alloys

Cobalt Alloys

Related Posts

Heat Exchanger Maintenance Checklist: How to Extend Equipment Life and Improve Performance

Heat Exchanger Maintenance

1. Introduction – Heat Exchanger Maintenance Checklist Following a structured heat exchanger maintenance checklist is the most effective way to keep your equipment running efficiently, avoid costly breakdowns, and extend service life. Whether you operate a shell and tube heat exchanger, a plate heat exchanger, or an air-cooled model, regular...

Read More
How to Choose the Right Tubular Heat Exchanger for Your Application

How to Choose

Selecting the appropriate tubular heat exchanger is a critical step for ensuring optimal thermal efficiency, mechanical integrity, and long-term operational reliability. As a widely used heat transfer device in process engineering, tubular designs—especially shell-and-tube heat exchangers—are the preferred choice for a wide variety of industrial applications. This article outlines the...

Read More
Export Packaging and Protection for Stainless Steel Heat Exchanger Tubes

Export Packaging and

When exporting stainless steel heat exchanger tubes, quality doesn’t stop at production—it must extend through to delivery. Improper packaging can result in corrosion, deformation, contamination, or mechanical damage during transit, especially over long sea voyages. At DLSS Pipeline, we ensure every shipment arrives in perfect condition with customized export packaging...

Read More
Integrated Stainless Steel Piping Solutions for Industrial Projects

Integrated Stainless Steel

Introduction In large-scale industrial projects—such as oil refineries, power plants, food processing lines, and chemical facilities—procurement teams often face a key challenge: how to consolidate material supply while ensuring technical compliance and on-time delivery. DLSS offers a complete stainless steel piping solution, including seamless pipes, fittings, flanges, and documentation services...

Read More
What is a Finned Tube and How It Improves Heat Exchanger Efficiency

Finned Tubes for

Finned tubes are widely used in heat exchangers, boilers, economizers, air coolers, condensers, evaporators, and heat recovery systems. Their main purpose is simple: increase the heat transfer surface area without greatly increasing the size of the equipment. However, finned tube selection is not only about adding more fins. A good...

Read More
desalination-projects-stainless-steel-heat-exchanger-tubes

How Global Desalination

With water scarcity on the rise, seawater desalination has become a critical infrastructure priority—especially in the Middle East, North Africa, Asia-Pacific, and parts of Latin America. These plants rely heavily on heat exchanger systems for energy-efficient freshwater production. And at the core of those systems? Stainless steel tubes that can...

Read More
How to Choose the Right Pipe Material for Your Industrial Project

How to Choose

Choosing the right pipe material is not only a purchasing decision. It affects corrosion resistance, pressure safety, temperature performance, welding, installation, maintenance cost, inspection, and long-term reliability. For industrial projects such as chemical plants, refineries, power plants, shipbuilding, heat exchangers, food processing, water treatment, and oil and gas systems, a...

Read More
Applications of Stainless Steel Seamless Pipes in the Shipbuilding Industry

Applications of Stainless

Introduction In modern shipbuilding—whether it’s a container vessel in Brazil, a naval patrol boat in Chile, or a passenger ferry in Argentina—material selection is critical. Exposure to saltwater, pressure, vibration, and corrosion demands high-performance piping systems. Stainless steel seamless pipes have become the go-to solution in many marine systems due...

Read More

Request A Quote

*We respect your confidentiality and all information are protected.